PDF p. 1599 · 2-2
Spot welding is also known as resistance spot welding, and it is the most suitable method of welding for vehicles. It has three main features: the welding can be performed instantaneously, it has a minimal effect on the source material, and it has a minimum effect on distortion to the absolute minimum. However for reliable results, please remember to remove all paint and other impurities from the surface of the material you intend to weld.
Welders:
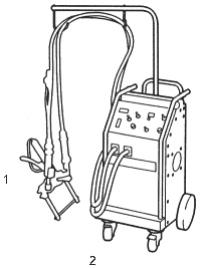
- 1. SPOT WELDER
- 2. TIMER/TRANSFORMER
Welding Conditions:
When performing spot welding, make sure that you conform to the following conditions: use the correct current, conductivity time, welding pressure, holding time, and shutdown time recommended for the spot welder.
Please bear in mind the following points when welding:
- Plate thickness and minimum welding pitch
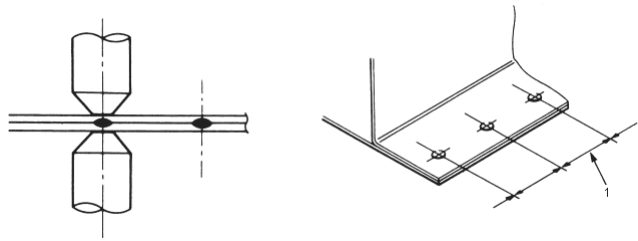
- 1. Intervals
NOTE: If the welding intervals are too short, branching may occur, making it impossible to maintain the desired soldering state. Unit: mm (in)
| Plate thickness | 0.6 (0.02) | 0.9 (0.04) | 1.2 (0.05) | 1.6 (0.06) |
| Minimum intervals | 11 (0.43) | 16 (0.63) | 20 (0.79) | 24 (0.94) |
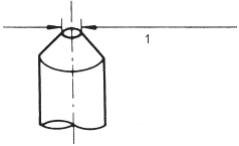
- 1. Tip Diameter
| Plate thickness | 0.8 (0.03) | 0.9 (0.04) | 1.2 (0.05) | 1.6 (0.06) |
| Tip diameter | 4.5 (0.12) | 5.0 (0.2) | 5.5 (0.22) | 6.0 (0.24) |
PDF p. 1600 · 2-3
Welding Strength Test
Even if you perform the welding according to the proper conditions, the strength of the welded sections may fluctuate due to drops in the voltage and other factors. The quality of the welding cannot be evaluated unless the welded sections are destroyed. Provide yourself with a steel plate of the same thickness and conduct a destruction test.
- If holes appear in the steel plates, it means that the welding is of standard strength.
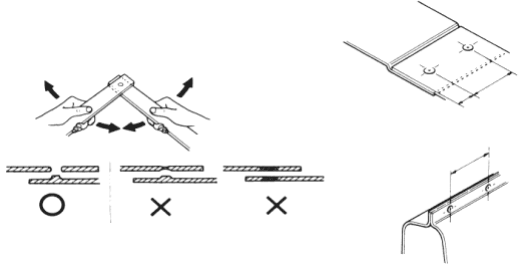
- Drive a wedge between two panels near the nugget. If the welded parts do not come apart and the diameter of the nugget is more than 3mm (0.1 in), the welding should be satisfactory.
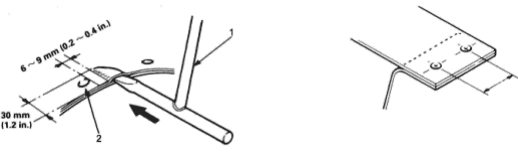
- 1. WEDGE
- 2. Stop inserting the wedge when the full size of the nugget appears
NOTE: It is difficult to perform spot welding in the following circumstances:
- When it is not possible to remove any rust or paint attached to the welding surfaces.
- When the tip of the spot welder cannot be inserted into the welding section.
- When the welding surfaces can be seen from the outside and welding will impair the exterior appearance.
In all these cases, the gas welding method should be employed. Moreover, if it is not possible to perform spot welding because of space restrictions, plug welding using the arc welding method may be performed instead. For plug welding, the sections to be welded must be closer together.